Precision-Engineered Disposable Syringes, Vacuum Filling Solutions, and Medical Consumables Built for Global Healthcare Systems and Contract Manufacturing.
Verified Sterile Medical Devices Engineered for Clinical Precision, Vaccine Delivery, and Automated Pharmaceutical Packaging Lines.
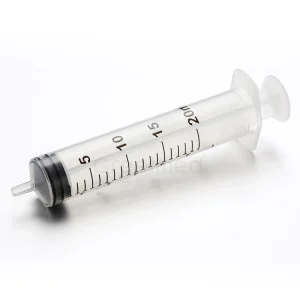
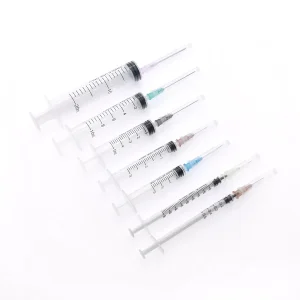
Hangzhou JZCare Medical Co., Ltd. is a professional medical consumables manufacturer specializing in disposable medical syringes, sterile injection devices, and high-quality healthcare disposable products for global medical markets. Established in 2011 and located in Hangzhou, China, the company integrates research and development, precision injection molding, automated production, sterilization processing, and global OEM/ODM services.
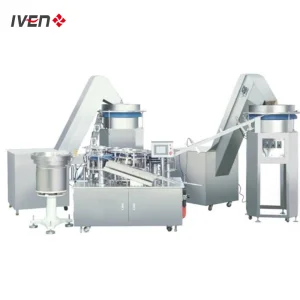
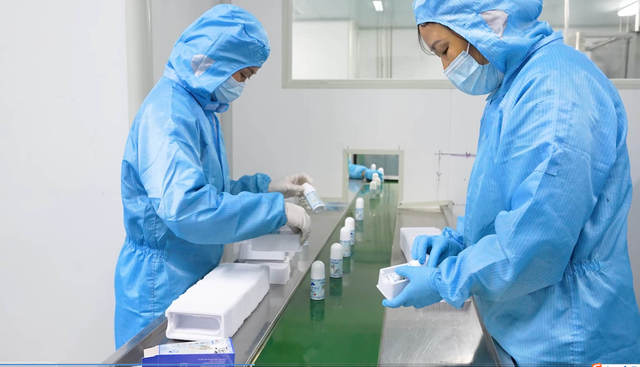
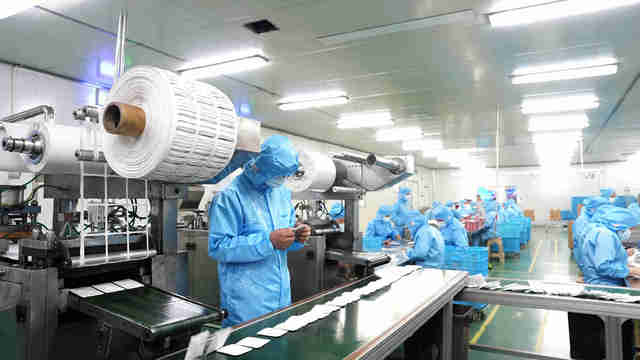
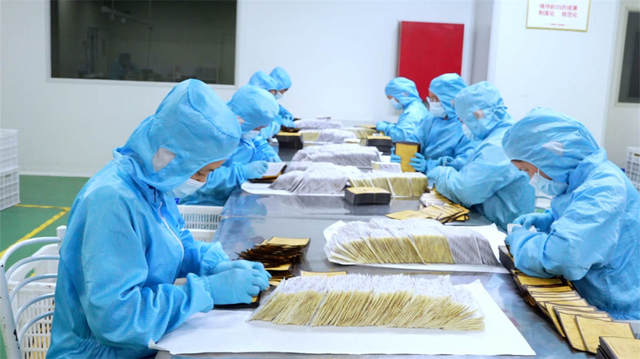
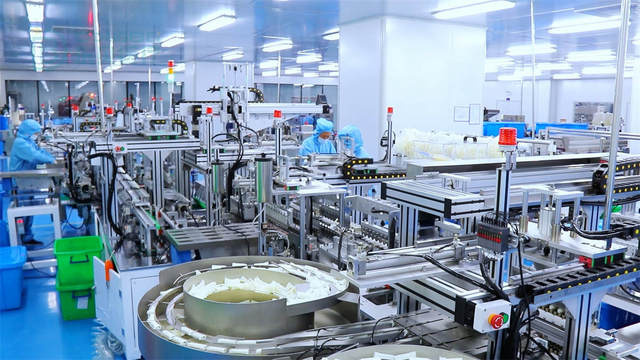
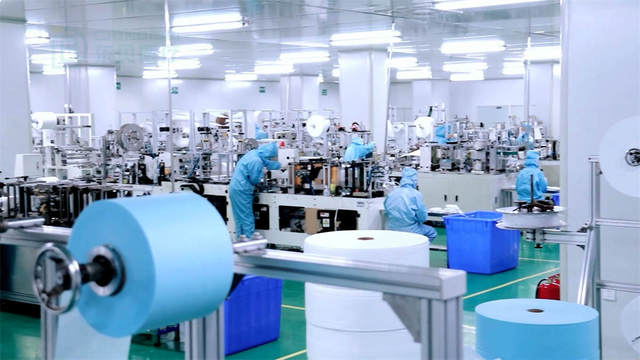
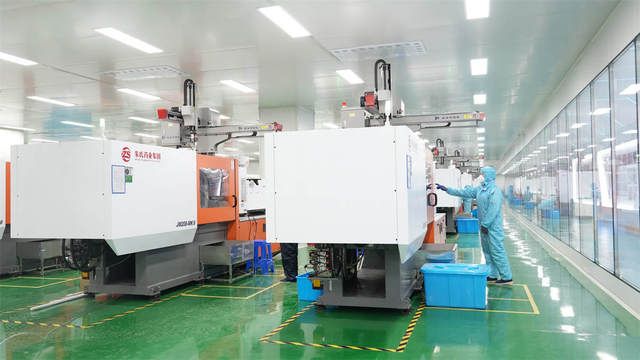
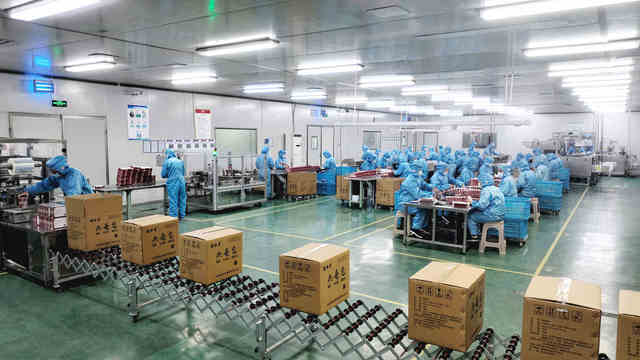
JZCare operates a modern manufacturing facility covering approximately 26,000 square meters with more than 300 employees, including experienced engineers, quality inspectors, and production specialists. The factory is equipped with advanced cleanroom workshops, fully automated assembly lines, and strict quality control systems to ensure product safety, consistency, and compliance with international medical standards. Annual production capacity exceeds 1.5 billion units of disposable medical products, supplying hospitals, clinics, laboratories, and healthcare distributors worldwide.
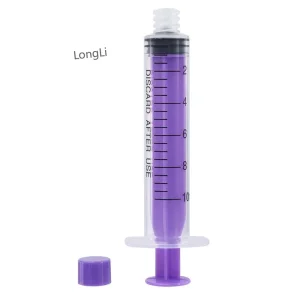
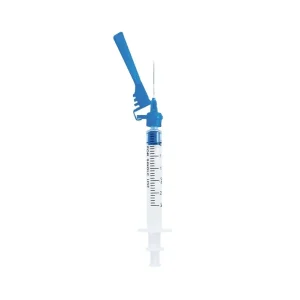
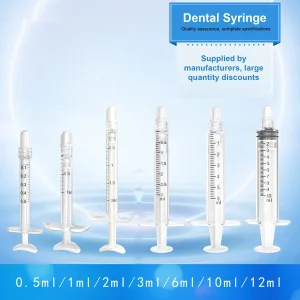
The company’s core product range includes disposable syringes, hypodermic syringes, safety syringes, insulin syringes, luer lock and luer slip syringes, and various sterile medical injection consumables. By adopting high-precision manufacturing technology, medical-grade materials, and rigorous sterilization processes, JZCare ensures reliable performance and patient safety in every product.
Driven by continuous innovation and global healthcare demand, Hangzhou JZCare Medical Co., Ltd. is committed to providing safe, efficient, and cost-effective medical disposable solutions while maintaining strong partnerships with international clients through stable quality, flexible customization, and professional service support.
Why leading global medical distributors, GPOs, and pharmaceutical brands centralize high-volume injection component production in East China.
Our localized supply chain in Zhejiang provides immediate access to virgin medical-grade Polypropylene (PP), ultra-pure Borosilicate 3.3 glass, and biomedical elastomer formulations, ensuring zero contamination and resilient cost control.
Deploying Class 100,000 cleanrooms integrated with robotics minimizes particulate burdens, human intervention, and bioburden levels, matching strict US FDA 510(k), CE MDR Class IIa, and ISO 7886 standards.
Generating over 1.5 billion injection units annually creates massive economies of scale, empowering global buyers to access tier-one dimensional precision and reliable batch stability at disruptive unit costs.
Engineered to meet diversified therapeutic needs across human medicine, intensive veterinary care, and high-speed robotic pharmaceutical bottling.
Engineered with zero-dead-space barrels to optimize vaccine utilization, preventing drug loss in critical high-volume immunization campaigns worldwide.
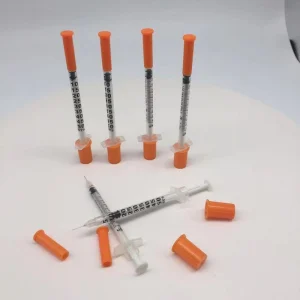
Ultra-fine cannulas (30G–32G) treated with medical silicone micro-coating ensure ultra-smooth skin penetration and precise insulin dose delivery for chronic diabetes regimens.
Heavy-duty barrels and high-impact plungers explicitly designed to withstand aggressive animal resistance in poultry, swine, and livestock medication administration.
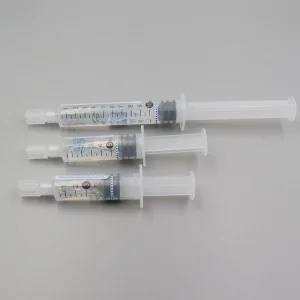
Medical-grade sterile prefilled saline flush systems minimize catheter occlusions and bloodstream infections in acute IV therapy workflows.
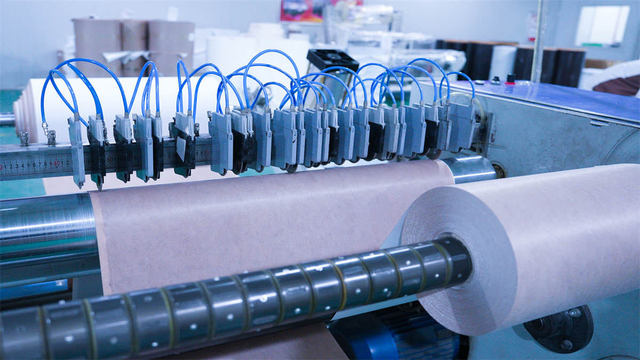
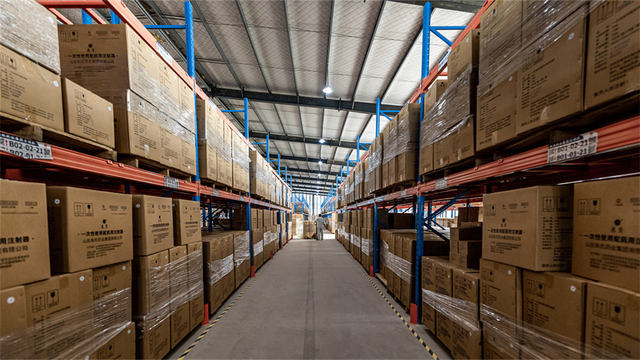
Explore our state-of-the-art 26,000 sqm production site equipped with automated assembly systems and rigorous QA laboratories.
In the procurement of Type B injection devices and medical consumables, multinational hospital groups, national tenders, and medical distributors prioritize strict regulatory compliance, low break-force tolerances, and structural integrity. A comprehensive supplier audit should systematically assess the following technical parameters:
1. Biocompatibility and Chemical Neutrality: Medical injection devices must comply fully with ISO 10993 (Biological Evaluation of Medical Devices). Materials such as polypropylene and synthetic rubber pistons must be evaluated for cytotoxicity, sensitization, intradermal reactivity, and systemic toxicity. At JZCare, raw materials are carefully checked for extractables and leachables to eliminate risks of interaction with active pharmaceutical ingredients (APIs).
2. Dimensional Conformity & Leak Resistance: Syringe barrels and plungers must strictly follow ISO 7886-1 and ISO 80369-7 (for 6% Luer tapers). Our multi-cavity hot-runner tooling maintains internal diameter tolerances within micrometers, preventing air ingress during aspiration and guaranteeing zero liquid leakage under sustained hydrostatic pressures exceeding 300 kPa.
3. Sliding Force Stability: High standard deviations in break-loose and sliding forces disrupt automated syringe pumps and cause inconsistent manual aspiration. Through precise silicone oil micro-misting technology, JZCare keeps plunger travel forces remarkably steady, improving both clinical ergonomics and safety in target dosing.
4. EO Sterilization Assurance Level (SAL 10⁻⁶): Our facility features automated ethylene oxide (EO) sterilization chambers that precisely manage preconditioning, temperature, humidity, gas concentration, and post-sterilization degassing cycles. Residual EO and ethylene chlorohydrin (ECH) levels are consistently maintained below 4 μg/g, fully complying with ISO 11135 limits.
Transparent solutions addressing compliance, supply chain logistics, customization, and factory production capacities.
Hangzhou JZCare operates under a certified ISO 13485:2016 quality management system. Our product lines hold CE certifications under the European MDR, full US FDA approvals, and complete compliance dossiers including biocompatibility reports (ISO 10993) and sterilization validation records (ISO 11135).
Yes. We support custom graduation scale markings (in ml, units, or proprietary dosing ratios), personalized barrel logo printing, customized plunger rod colors, specialized needle bevel configurations, and individual blister or ribbon packaging solutions adapted to your target regulatory requirements.
Standard MOQs start at 50,000 to 100,000 units depending on the device caliber and packaging configurations. Regular container-load production schedules typically conclude within 25–35 days from sample sign-off and deposit confirmation, backed by an annual factory throughput exceeding 1.5 billion units.
Our barrels are engineered with reinforced dual-locking retaining rings at the rear flange to eliminate inadvertent plunger pullout during aspiration. Furthermore, our high-elasticity synthetic rubber plungers feature dual sealing collars designed using FEA fluid models to maintain leak resistance at high backpressures.
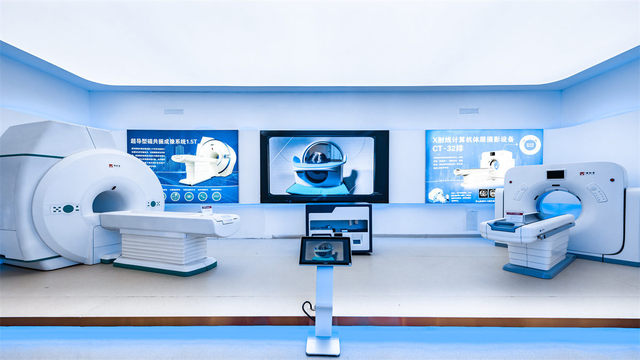
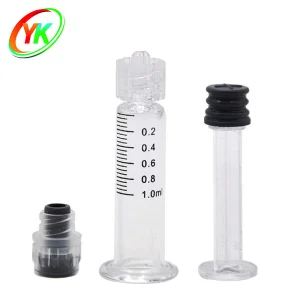
High-Precision Borosilicate Syringes, Safety Tuberculin Consumables, Prefilled Flush Syringes, and Imaging Radiography Solutions.
 JZCare Syringe